

Email: sales@prodrill.com.cn
Tel:0086-18959243380
Addr: Room 805 C1 Wanda Plaza, No.5 Jinzhong Road, Huli District, Xiamen, China
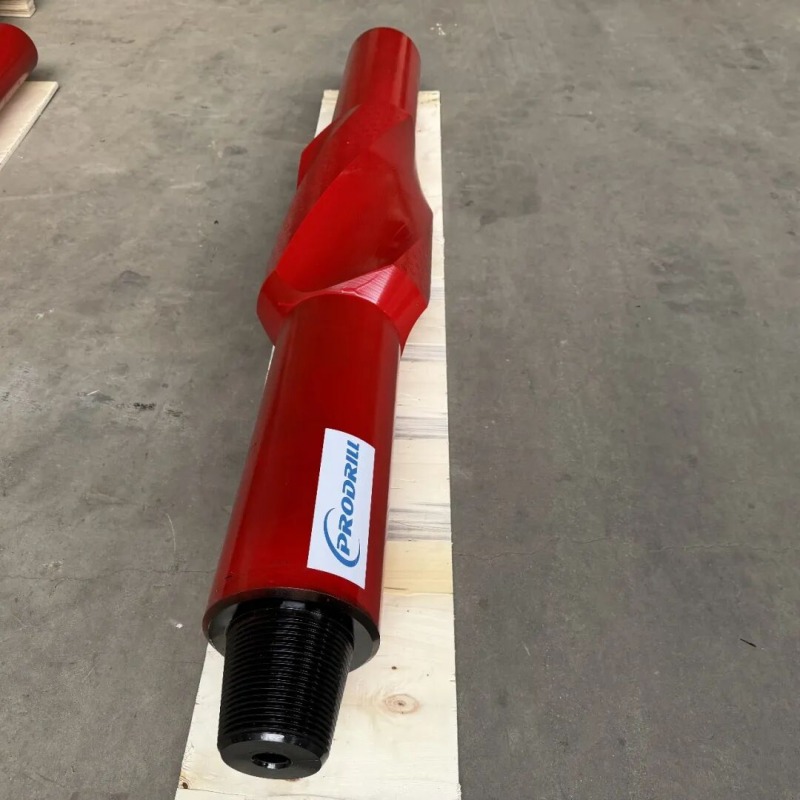
High-quality custom-made Integraled Spiral Strip Stabilisers, crafted with meticulous attention to detail, showcasing "Made in China" to the world
26 Oct 2026
If you think that drilling tool manufacturing is just simple "forging," then you're mistaken. Behind this batch of ProDrill integral spiral wear-resistant belt Integraled Spiral Strip Stabilisers, soon to be shipped to Perth, Western Australia, lies precise and meticulous 3D modeling and a manufacturing process refined through countless trials.
Experienced oil drilling professionals know that in the complex conditions of deep and ultra-deep wells, Integraled Spiral Strip Stabilisers are the "stabilizing force" of the drill string. This batch of Integraled Spiral Strip Stabilisers, custom-made for Australian clients , is manufactured to stringent standards, showcasing ProDrill's expertise in downhole tool manufacturing.
First, watch the video on the video account:
1. Robust OD 240MM outer diameter
Its extra-large 240mm outer diameter means it can provide strong support and anti-skewness straight-line drilling capabilities downhole. Look at the clear spiral band on its surface, and the dense "diamond" pattern on it—that's our carbide wear-resistant band! Under high-speed rotation and intense friction, this "armor" can greatly extend the tool's service life, fearless of hard formations.
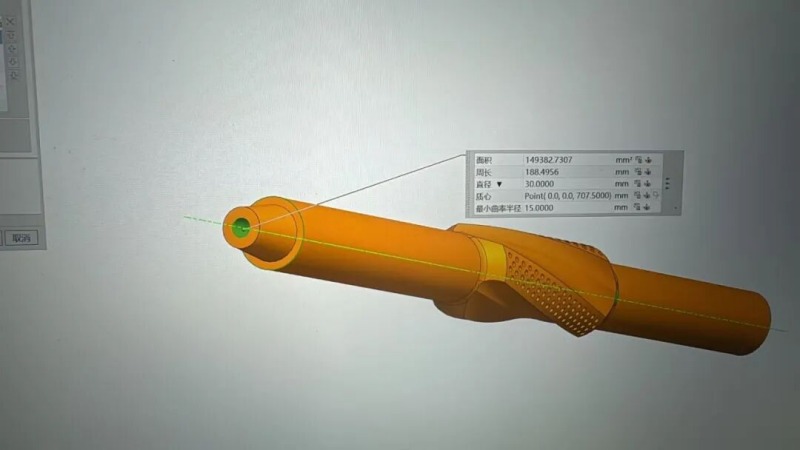
2. Unique "30mm continuous inner hole" design
One of the biggest highlights of this order is the 30mm internal hole (30mm inner diameter) requested by the customer. Take a look at the previous quality inspection photos: Our engineers provided a CAD 3D design (see below), and the software accurately calculated the diameter to be 30.0000 mm. This is precisely the core technical parameter strongly requested by the Australian customer – 30mm internal hole (30mm inner diameter).
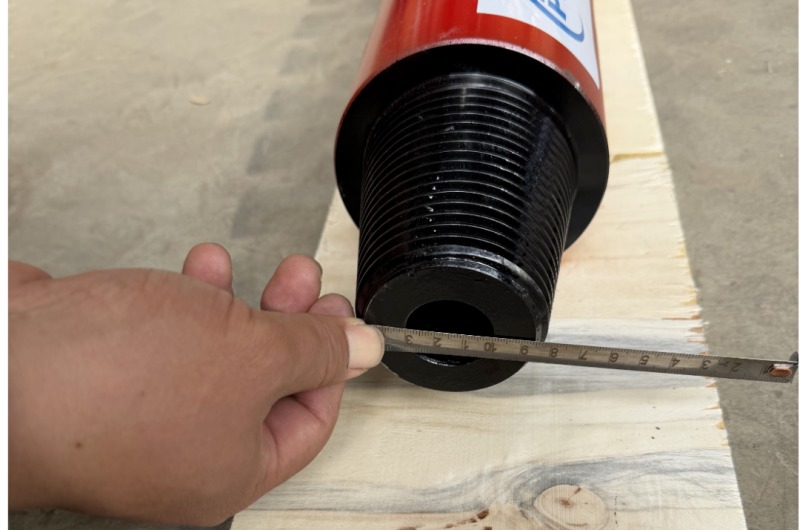
As the saying goes, "A small error can lead to a huge mistake." In complex working conditions such as deep wells and ultra-deep wells, every parameter of the centralizer is related to the safety and efficiency of drilling.
The inner bore is precisely penetrated to meet the needs of special fluid circulation or cable threading in downhole. Both ends are equipped with standard 4 ½ API REG PIN BOX connectors for seamless compatibility with mainstream drilling tools.
The effective length is 1.5M and it has a continuous 30mm internal passage.
This design not only ensures smooth flow of drilling fluid and reduces pressure drop, but also effectively prevents rock cuttings from accumulating and getting stuck in the inner hole, making it an extremely ingenious design .
From the precise 30.0000mm inner hole on the 3D drawings to the bright "PRODRILL red" in the workshop, this is not just the birth of a downhole tool, but also the ultimate refinement of "craftsmanship" in Chinese manufacturing.
at how many manufacturing hurdles and technical challenges a high-quality, custom-made Integraled Spiral Strip Stabilisers must overcome.
To meet the stringent requirements of Australian customers for complex geological formations (4 ½ API REG PIN BOX connectors, 30mm inner diameter, and a continuous 1.5M effective length channel), the factory's R&D and production teams undertook a rigorous technical challenge .
Challenge 1: The meticulously prepared blank and the "narrow window" heat treatment
Pain point: The stress in the well is extremely complex, and spliced parts or forgings with interlayers or loose structure are very prone to breakage when placed in the well.
Key breakthrough: We strictly reject any welded or spliced parts, and use 4145H/42CrMo high-strength alloy structural steel for integral forging.
In the subsequent quenching and tempering heat treatment, engineers precisely targeted the "narrow window": too high a hardness would lead to brittle fracture, while too low a hardness would result in rapid downhole wear. Only by achieving the ultimate in metallographic structure and hardness uniformity could it be endowed with the soul of "a balance of rigidity and flexibility".
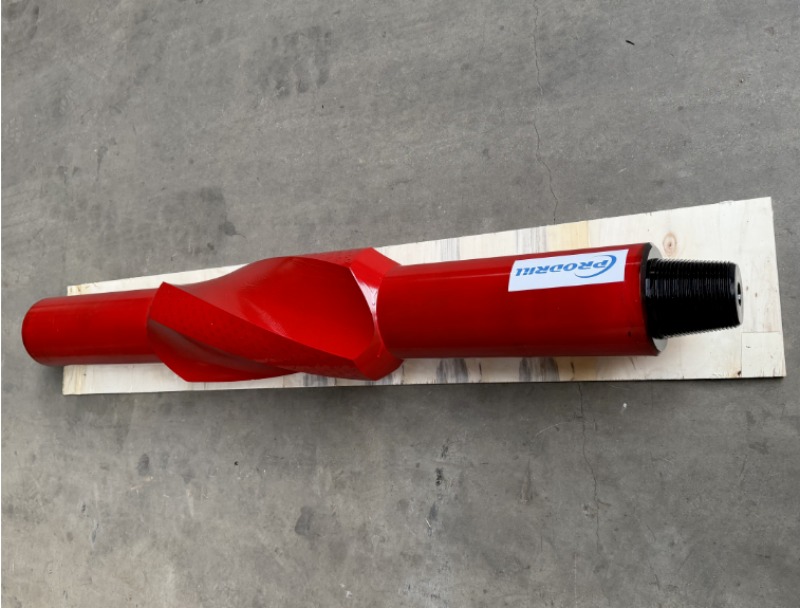
Challenge 2: Five-axis linkage challenges "continuously changing helix angles"
Pain point: The spiral cutter blade is a complex curved surface with continuously changing angles, which ordinary lathes are simply incapable of handling. If the angle deviates even slightly, the drilling fluid flow field will become turbulent, leading to poor cuttings carrying capacity, pressure buildup, or even stuck drill bit.
Key breakthroughs: We employed high-precision four-axis/five-axis CNC milling machines, strictly adhering to the hydraulic model design for milling. This ensured absolute uniformity in the helix angle and cutter blade thickness, preventing eccentric stress on the centering support, effectively suppressing drill string vibration, and precisely controlling well inclination.
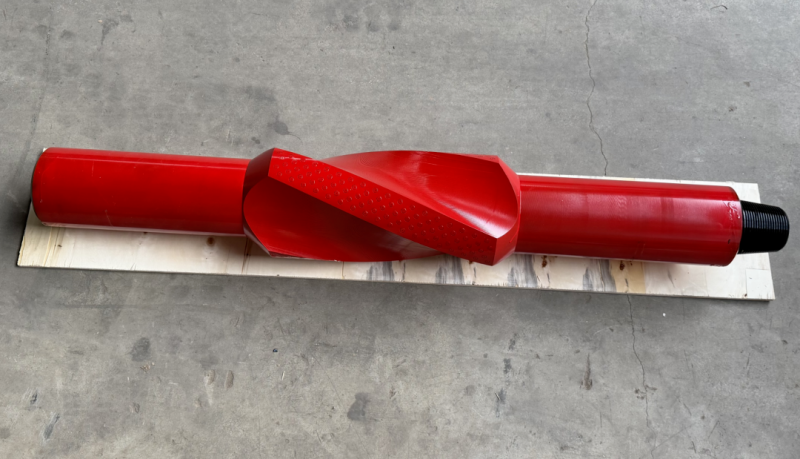
Challenge 3: The "A Song of Ice and Fire" of Wear-Resistant Layer Welding (Core Challenge)
Pain point: The thermal expansion coefficients of the base steel and tungsten carbide differ greatly, and improper temperature control can easily lead to thermal cracking, peeling, and flaking.
Key Technology: Take a close look at the densely packed dotted texture on the blades of our product—this is our core technology. We employ advanced plasma spraying and PTA automatic cladding technology, specifically designed for high-end products. This allows for strict temperature control while minimizing dilution. As a result, the wear-resistant layer and the substrate bond seamlessly, leading to a dramatic increase in hardness and completely eliminating chipping and peeling.
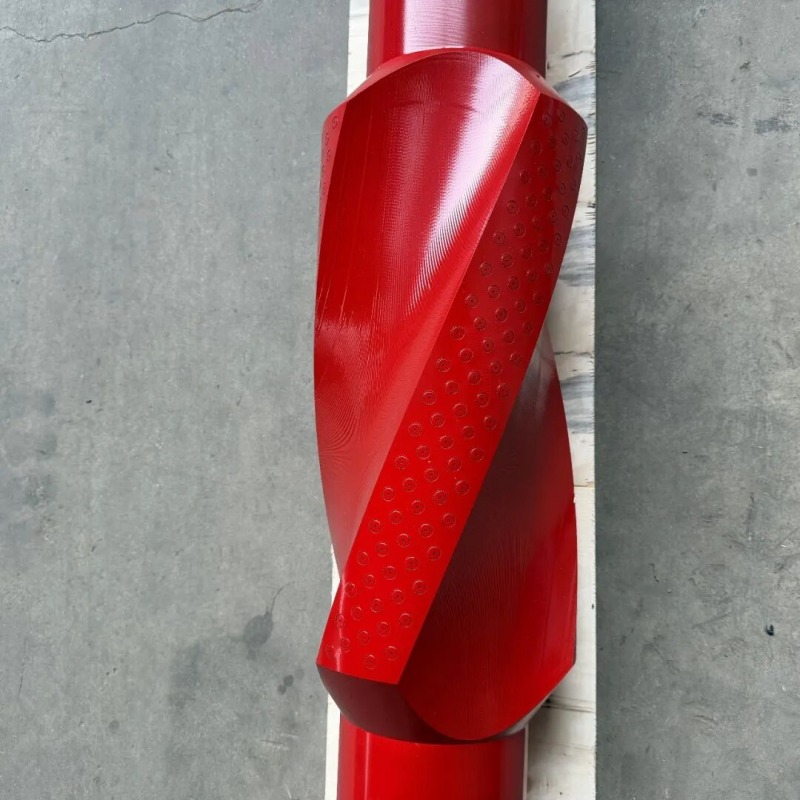
Challenge 4: APL Standard Threads and the "Flaw Detection Test"
Pain point: Long workpieces are prone to deformation during machining, and internal hidden cracks are the main culprit for tool breakage. Many small factories get stuck at this hurdle.
Technical breakthroughs: Our 4 ½ API REG PIN BOX connector strictly adheres to API standards, with extremely high precision in tooth profile, taper, and sealing surface.
At the same time, finished products must undergo dual "physical examinations" of MT magnetic particle testing and UT ultrasonic testing before leaving the factory, nipping any potential coaxiality tolerances and internal cracks in the bud.
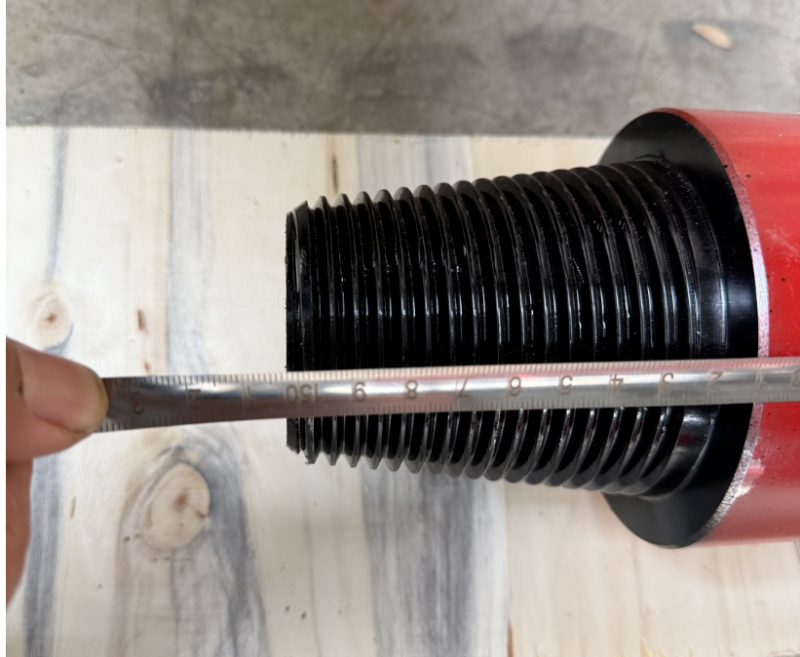
Challenge 5: Rejecting superficial imitations, hydraulic simulation is the definitive answer.
Pain points: The spiral structure is asymmetrical, resulting in large high-speed centrifugal vibration; aftermarket parts only imitate the outer shell, causing severe grinding against the well wall after being run into the well.
Technical breakthroughs: Before mass production, each batch of ProDrill Integraled Spiral Strip Stabilisers undergoes rigorous hydraulic simulation verification and dynamic balancing tests. This not only verifies the annular flow velocity and cuttings backflow capability, but also ensures smooth and unobstructed mud flow with lower pressure drop under continuous 30mm inner bore penetration.
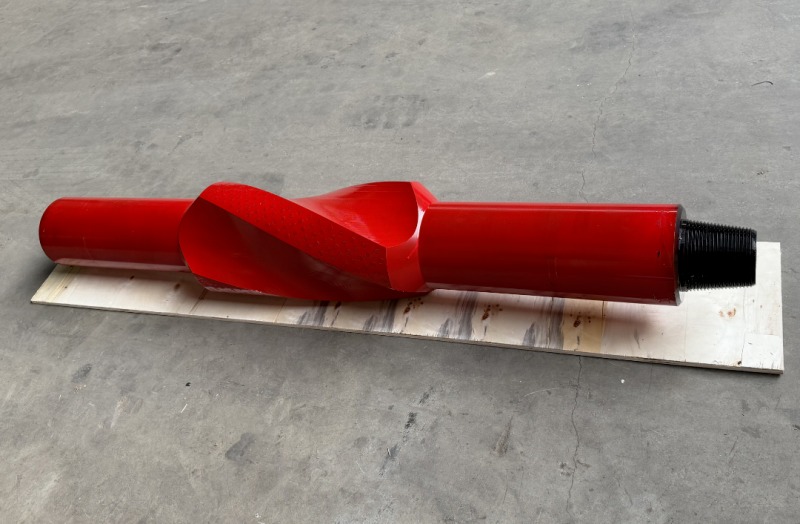
Australian mining is known for its stringent standards and complex operating conditions. To secure and deliver this order on time, our team rigorously controlled every step, from confirming drawings and cutting raw materials to precision machining, welding wear-resistant belts, and applying high-quality red anti-corrosion paint.
This is more than just a simple shipment; it's a powerful demonstration of the core strength of Chinese manufacturing in the Southern Hemisphere. We deeply understand that only by perfecting every product can we earn the long-term trust of our international customers.
As a professional downhole tool manufacturer, ProDril is committed to providing high-quality drilling solutions to customers worldwide. Whether it's integral auger Integraled Spiral Strip Stabilisers, drill collars, or other downhole tools, we can provide professional customized solutions for any special specifications (outer diameter, inner bore, length, thread type).
ProDrill, conquering the world with great products, we're always on the move!